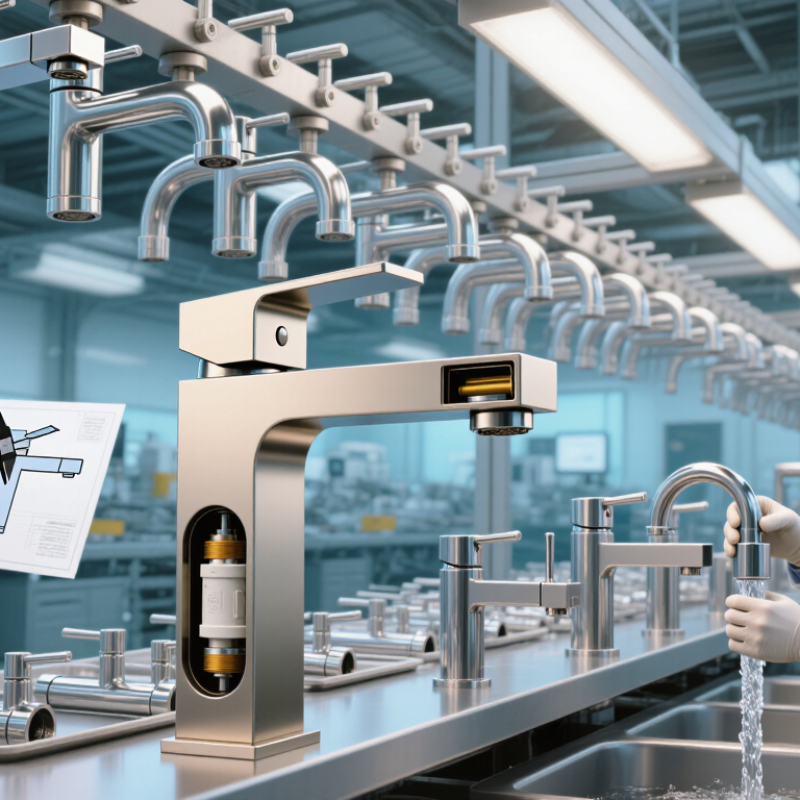
| OEM Manufacturer Role | An OEM manufacturer develops and produces a faucet according to a buyer’s specifications, which may include geometry, materials, finishes, packaging, testing, and production tolerances. | It enables a luxury brand, distributor, or project supplier to control product appearance and performance without owning the complete manufacturing operation. | Review approved drawings, bills of materials, control plans, inspection records, and product samples. |
| Primary Faucet Body Material | Plumbing brass is commonly used for faucet bodies, valves, spouts, and connectors because it is machinable, corrosion resistant, and suitable for pressure-containing components. | Material selection affects structural reliability, machining quality, corrosion resistance, weight, and the final tactile impression of the faucet. | Check the material specification, supplier certificates, incoming inspection records, and alloy composition test results. |
| Lead-Content Benchmark | For products covered by the U.S. Safe Drinking Water Act “lead-free” definition, the weighted average lead content of wetted surfaces must not exceed 0.25%. | This is a key market-access requirement for faucets intended for potable-water applications in the United States and other markets that reference similar limits. | Use an applicable certification or laboratory report and verify that the tested configuration matches the production model and wetted materials. |
| Wetted Components | Wetted parts may include the body, valve housing, cartridge interface, aerator housing, flexible connectors, and internal water passages. | Compliance cannot be assessed from the visible outer body alone; every material in contact with drinking water may influence extraction results. | Prepare a complete wetted-materials list and maintain traceability for each component and revision. |
| Stainless-Steel Alternative | Stainless steel can be specified for selected faucet components where high corrosion resistance, a different visual character, or reduced lead risk is required. | It may support premium positioning, but machining behavior, surface finishing, cost, and component design must be evaluated before substitution. | Confirm the specified stainless-steel grade, surface condition, corrosion testing, and compatibility with valves and other components. |
| PVD Finish Technology | Physical Vapor Deposition deposits a thin, hard coating in a vacuum environment. Common decorative coating families include titanium-, zirconium-, and chromium-based systems. | PVD can provide a durable metallic appearance with improved resistance to wear and surface discoloration compared with many conventional decorative finishes. | Verify the coating system, base-metal preparation, process parameters, color standard, and performance test results. |
| PVD Coating Thickness | Decorative PVD thickness is process-dependent and is often specified in micrometres rather than by appearance alone. A project specification should define the minimum acceptable thickness and test method. | Thickness, adhesion, substrate preparation, coating chemistry, and geometry jointly affect durability; thickness alone is not a complete quality indicator. | Use calibrated coating-thickness measurement, coating-adhesion testing, and production-sample inspection. |
| Surface Preparation | Polishing, cleaning, degreasing, and activation of the substrate are essential before PVD deposition. Surface defects may remain visible through a thin decorative coating. | Premium finishes require consistent gloss, uniform color, low surface roughness, and controlled edge and corner treatment. | Inspect under standardized lighting and use agreed samples, gloss requirements, color tolerances, and visual defect limits. |
| Finish Durability | Typical evaluations may include abrasion, chemical-resistance, humidity, salt-spray, adhesion, and cyclic corrosion tests. The exact method and acceptance level depend on the destination market and project specification. | Luxury faucets are frequently exposed to water, soap, cleaners, fingerprints, and repeated handling, so decorative durability must be validated rather than assumed. | Require third-party or internal laboratory reports that identify the test method, sample construction, exposure duration, and pass criteria. |
| NSF/ANSI/CAN 61 Scope | NSF/ANSI/CAN 61 evaluates the health effects of materials and components that contact drinking water, including potential contaminant extraction under defined conditions. | It addresses material safety for potable-water contact; it is not a general replacement for mechanical, dimensional, pressure, or decorative-finish testing. | Confirm the applicable product category, test configuration, formulation records, and current certification or evaluation documentation. |
| Certification Interpretation | Compliance or certification applies to the tested product scope, materials, manufacturing location, and configuration identified in the relevant documentation. | A change to the alloy, cartridge, hose, seal, coating, supplier, or production site may require a technical review or additional testing. | Use engineering-change control and obtain written confirmation before making changes to certified or evaluated components. |
| Pressure Performance | Faucets should be evaluated against applicable plumbing standards for pressure integrity, leakage, flow performance, and operating cycles. Requirements vary by product type and market. | A faucet may have compliant drinking-water-contact materials but still fail because of leakage, valve wear, poor connections, or inadequate pressure resistance. | Conduct type testing and production audits using the standards specified for the target market and faucet category. |
| Cartridge and Seal Materials | Cartridges, elastomeric seals, washers, hoses, and aerators are functional and potentially wetted components that require compatibility with water, temperature, pressure, and cleaning conditions. | These parts strongly influence service life, drip prevention, flow stability, and the overall compliance profile of the finished faucet. | Maintain approved-component lists, material declarations, incoming inspection, endurance testing, and revision control. |
| OEM Quality-Control Package | A robust package commonly includes approved drawings, material certificates, inspection standards, process-control records, laboratory reports, traceability data, and packaging specifications. | Documented controls make it easier to reproduce the approved design across production batches and to investigate field issues. | Audit the document-control system and compare mass-production samples with the approved golden sample. |
| Recommended Procurement Requirement | Specify the alloy or material, lead-content limit, wetted-component list, PVD color and performance criteria, applicable potable-water requirements, pressure tests, sampling plan, and change-notification procedure. | A measurable specification reduces ambiguity, limits unauthorized substitutions, and aligns design, compliance, production, and purchasing teams. | Include all requirements in the technical agreement, quality agreement, inspection plan, and pre-production approval process. |