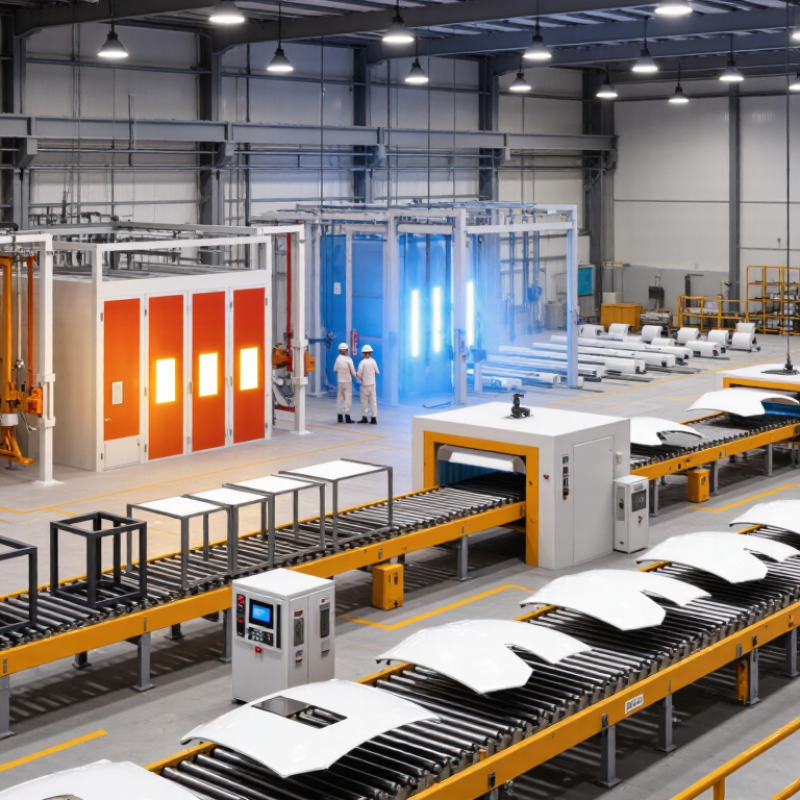
| 1 | Conveyorized Spray Painting Line | Metal cabinets, appliances, automotive components, fabricated parts | Air spray, airless spray, or electrostatic spray | Small to medium parts; generally up to approximately 2 m in length | Approximately 100–600 parts per shift, depending on size and curing time | High and consistent | Medium- to high-volume production with repeated part geometries | Continuous material flow and stable coating thickness | Less flexible for frequent product changes |
| 2 | Electrostatic Liquid Painting Line | Steel frames, automotive parts, machinery housings, metal furniture | Electrostatically charged liquid paint with grounded workpieces | Small to medium metal components | Approximately 150–800 parts per shift | Very high transfer efficiency | Conductive metal parts requiring uniform decorative or protective coating | Lower overspray and improved paint utilization | Requires suitable grounding and controlled paint conductivity |
| 3 | Powder Coating Line | Metal furniture, electrical enclosures, wheels, profiles, outdoor equipment | Electrostatic powder spraying followed by oven curing | Small parts to long profiles, depending on booth and oven layout | Approximately 150–1,000 parts per shift | Durable and uniform | Metal products needing strong abrasion, corrosion, and weather resistance | High coating utilization and no solvent evaporation | Unsuitable for heat-sensitive substrates and some very thin films |
| 4 | Dip Coating Line | Small metal parts, wire goods, fasteners, agricultural components | Parts immersed in a liquid coating tank and withdrawn at controlled speed | Small to medium parts with accessible surfaces | Approximately 200–2,000 parts per shift | Good coverage on complex shapes | Parts requiring internal and recessed-area coverage | Simple process and effective coverage of irregular geometries | Drainage marks and variable film thickness may occur |
| 5 | Electrophoretic Painting Line | Automotive bodies and components, chassis parts, metal assemblies | Water-based electro-deposition using an electrical current | Small components to complete vehicle bodies | Approximately 20–120 bodies or equivalent loads per hour | Excellent corrosion protection | High-volume metal manufacturing requiring reliable primer coverage | Uniform coating in cavities and recessed areas | High capital cost and strict bath-control requirements |
| 6 | Roller Coating Line | Coil steel, aluminum sheets, panels, composite boards | Metered roller application on continuous sheet or strip | Continuous flat materials, commonly 0.5–2.0 m wide | Approximately 20–150 m/min, depending on coating and curing system | Highly uniform on flat surfaces | Continuous coil-coating and panel production | High speed, precise film control, and low overspray | Not suitable for three-dimensional or highly irregular parts |
| 7 | Curtain Coating Line | Wood panels, doors, flooring, flat furniture components | Continuous curtain of coating falling onto horizontally moving panels | Flat boards and panels, commonly up to approximately 1.3 m wide | Approximately 5–40 m/min | Smooth and consistent on flat panels | High-volume wood and panel finishing | Fast application with consistent coverage across panel width | Requires flat, stable workpieces and carefully controlled viscosity |
| 8 | Automatic Reciprocating Spray Line | Doors, cabinets, profiles, appliances, medium-sized fabricated parts | Programmable spray guns moving vertically or horizontally | Medium and large parts with repeatable dimensions | Approximately 40–250 parts per shift | Consistent with programmable recipes | Mixed production requiring automation without a fully dedicated line | Good balance between flexibility and labor reduction | Lower output than fully continuous high-speed systems |
| 9 | Manual Spray Booth Line | Custom metalwork, prototypes, repair parts, low-volume products | Operator-controlled air, airless, or HVLP spray application | Small parts to large structures, subject to booth capacity | Approximately 10–100 parts per shift | Dependent on operator skill | Low-volume, high-mix, oversized, or frequently changing products | High flexibility and relatively low initial investment | Greater labor dependence and wider variation in finish quality |
| 10 | UV-Curing Painting Line | Wood flooring, furniture panels, decorative boards, printed surfaces | UV-curable coating followed by ultraviolet lamp curing | Flat wood and composite panels | Approximately 5–30 m/min, depending on coating formulation | Hard, fast-curing surface | Interior panels requiring rapid handling and high scratch resistance | Very short curing time and high production density | Requires UV-compatible coatings and controlled lamp maintenance |